
CNC machining uses computer-controlled cutting tools to make titanium eyeglass frame parts from stock. These can include fronts, temples, bridges, end pieces, hinges, and rimless hardware. The process can suit complex contours, repeatable holes, or small runs that do not justify a dedicated stamping die. CNC alone does not guarantee quality. Results depend on the alloy, drawing, toolpath, fixture, cutting tools, process controls, and inspection plan. This guide explains the process and what buyers should ask to see.
What does CNC machining mean?
CNC stands for computer numerical control. An engineer defines the part geometry and tolerances in a CAD model or drawing. A programmer then uses computer-aided manufacturing, or CAM, software to create toolpaths. The machine controller executes those programmed movements while tools cut the workpiece.
The program can control tool position, feed, spindle speed, coolant, and tool changes. It cannot correct a vague tolerance or a poorly defined datum. The machine follows the program, even when the specification needs revision.
This distinction matters: CNC describes how a machine is controlled, not one material or one cutting method. CNC equipment includes mills, lathes, drills, grinders, and wire electrical discharge machines. For eyewear, CNC milling is usually the most visible process because it can shape a complete front or temple from plate or bar.
The US National Institute of Standards and Technology explains that CAM systems create toolpaths from part geometry and expert process input, while the CNC system executes the machining commands. That human process knowledge remains important even on advanced equipment. See NIST’s review of integrated CAM and CNC control.
Which eyeglass frame parts can be CNC machined?
Manufacturers can machine several titanium eyewear components:
- a one-piece front with rims, bridge, and end pieces;
- separate rims, bridges, or end pieces for later joining;
- temples with tapered sections, decorative pockets, or integrated hinge features;
- nose-pad arms, hinge blocks, pins, screws, bushings, and rimless mounting parts;
- jigs, gauges, and assembly fixtures used to make the frame.
A frame advertised as CNC machined may contain only one CNC-made part. Ask which components are machined, from what stock, and which later operations change them.
Some frames use a combination of processes. A factory may laser-cut a rough front, CNC-machine the lens interfaces and hinge areas, form the bridge, weld separate features, polish the surfaces, and then apply a coating. This lets the manufacturer select a process for each feature.
Our titanium eyewear guide explains how material, construction, joining, and finishing work together in a finished frame.
How CNC machining for titanium eyeglass frames works
The sequence depends on the design, but these are the main stages to review.
1. Specify the titanium stock
The drawing should identify the material by grade, applicable specification, product form, and condition. “Titanium” alone is not a purchase specification.
Plate, sheet, bar, and billet can have different dimensional limits and processing histories. ASTM’s current B265 specification covers annealed titanium and titanium-alloy strip, sheet, and plate. Bar or billet projects may use a different specification. The supplier should connect the incoming certificate to the production lot.
Commercially pure grades and titanium alloys also cut differently. Do not copy settings from one grade to another without validation. Read our comparisons of pure titanium eyewear and titanium alloy eyewear before approving a material substitution.
2. Review the CAD model and drawing
The engineering review defines datums, critical dimensions, tolerances, edge breaks, threads, surface requirements, and inspection methods. It also checks whether tools can reach every feature and whether the part stays stiff enough during cutting.
Thin rims and temples need particular attention. A feature may look elegant in CAD but deflect under cutting force or become fragile after polishing. Engineers may adjust the machining sequence, add temporary support, or leave extra material for a later finishing pass.
3. Create and simulate the CAM toolpaths
The programmer selects tools and builds the operation sequence. Roughing removes most of the stock. Semi-finishing stabilizes the shape. Finishing passes create the controlled dimensions and visible surfaces.
CAM simulation checks for collisions, excess stock, missed areas, and unexpected machine movement. It does not replace first-article inspection because a simulation cannot account fully for real tool runout, fixture movement, heat, burrs, or tool wear.
4. Build a stable fixture
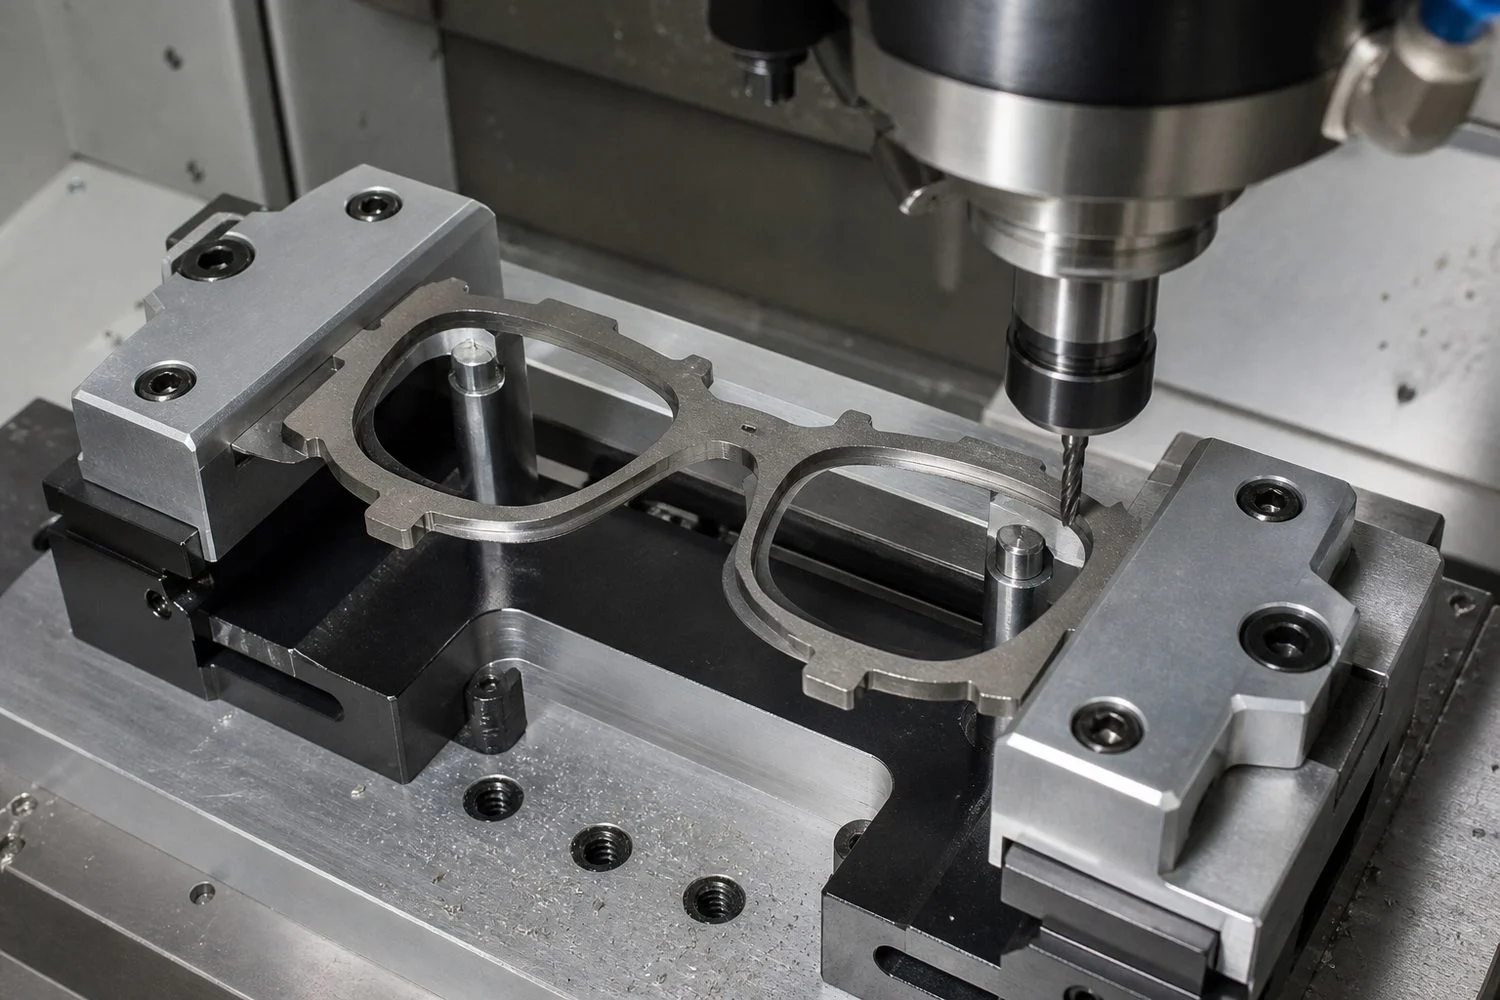
Workholding controls where the part sits and how cutting forces enter it. A thick blank is easier to hold than a nearly finished frame with thin rims and narrow bridges.
Custom soft jaws, nests, vacuum fixtures, tabs, or sacrificial support features may be used. The fixture should locate the same datums on every cycle without marking a cosmetic surface. If the part needs a second setup, the transfer method must preserve alignment between the two sides.
Five-axis machining can improve access and reduce reclamping for complex geometry. It does not automatically create tighter tolerances. Machine condition, tool length, thermal stability, probing, fixturing, and process validation still set the practical result.
5. Machine the part with controlled cutting conditions
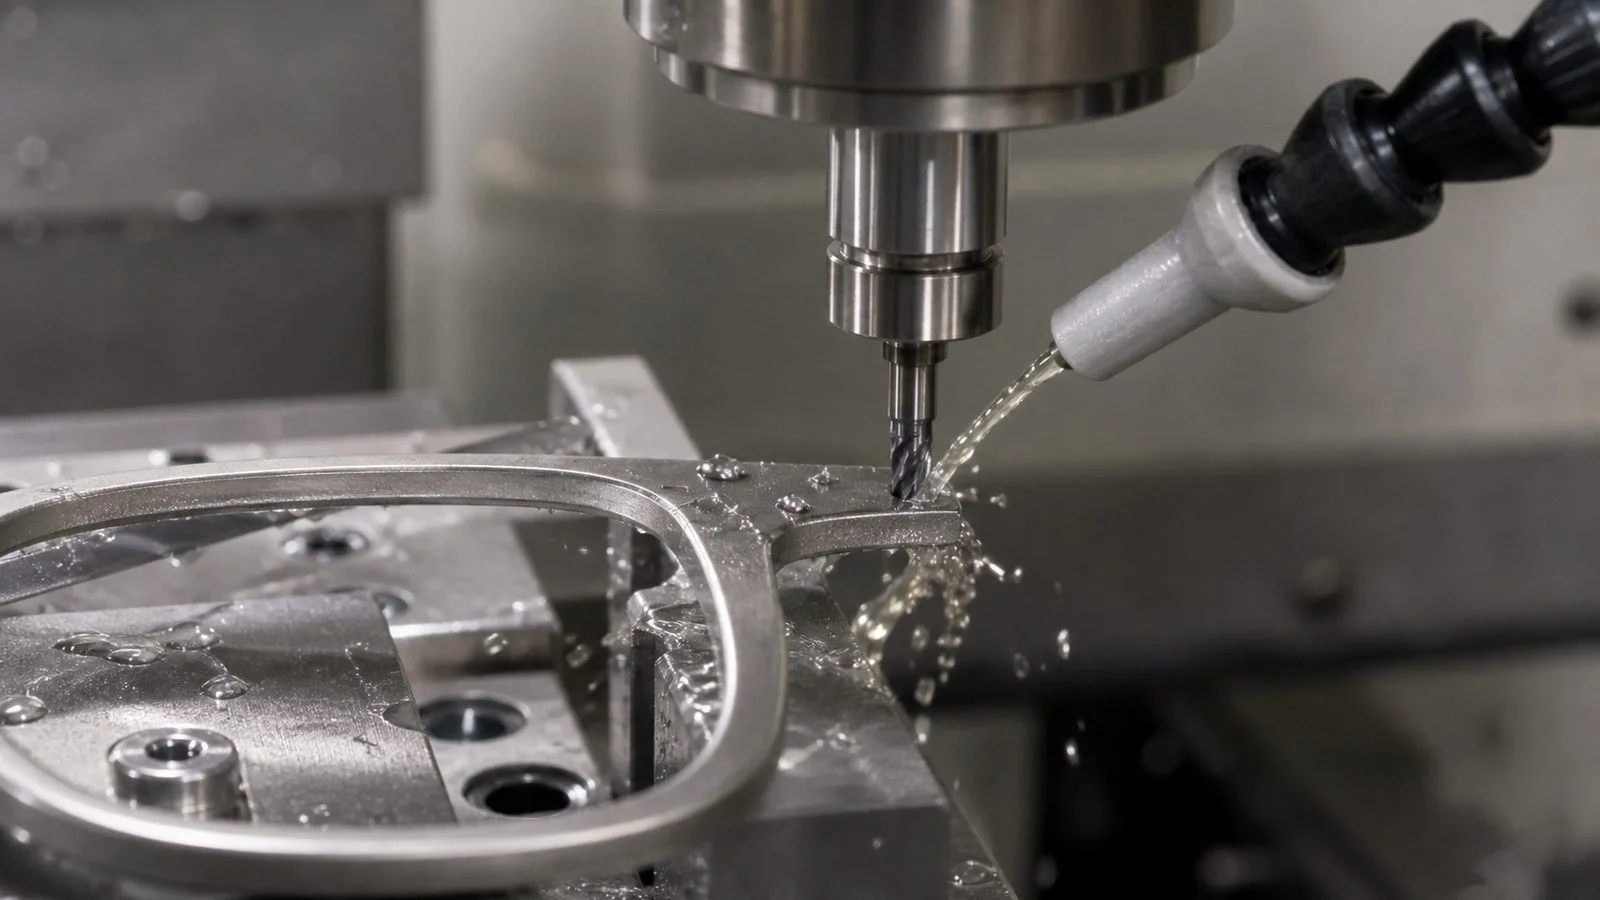
The factory selects tool geometry, cutting speed, feed, depth of cut, coolant delivery, and tool engagement for the exact titanium grade and setup. A rigid machine and sharp tools help maintain a clean, consistent cut.
Roughing and finishing have different goals. Roughing removes stock efficiently without creating unstable heat or vibration. Finishing protects critical dimensions and the surface that polishing must later refine. A tool that remains usable for roughing may no longer be suitable for a visible finishing pass.
6. Deburr, clean, and prepare the surface
Machining can leave sharp edges, burrs, tool marks, and trapped chips. Deburring removes unwanted edges without rounding a controlled feature or thinning the frame unevenly. Cleaning removes coolant and residue before welding, polishing, or coating.
Polishing can alter dimensions. Lens grooves, screw seats, rimless holes, and mating faces may need protection or a defined polishing allowance. A dimensional report taken before aggressive polishing does not prove the finished part still meets the drawing.
7. Inspect the first article and production lot
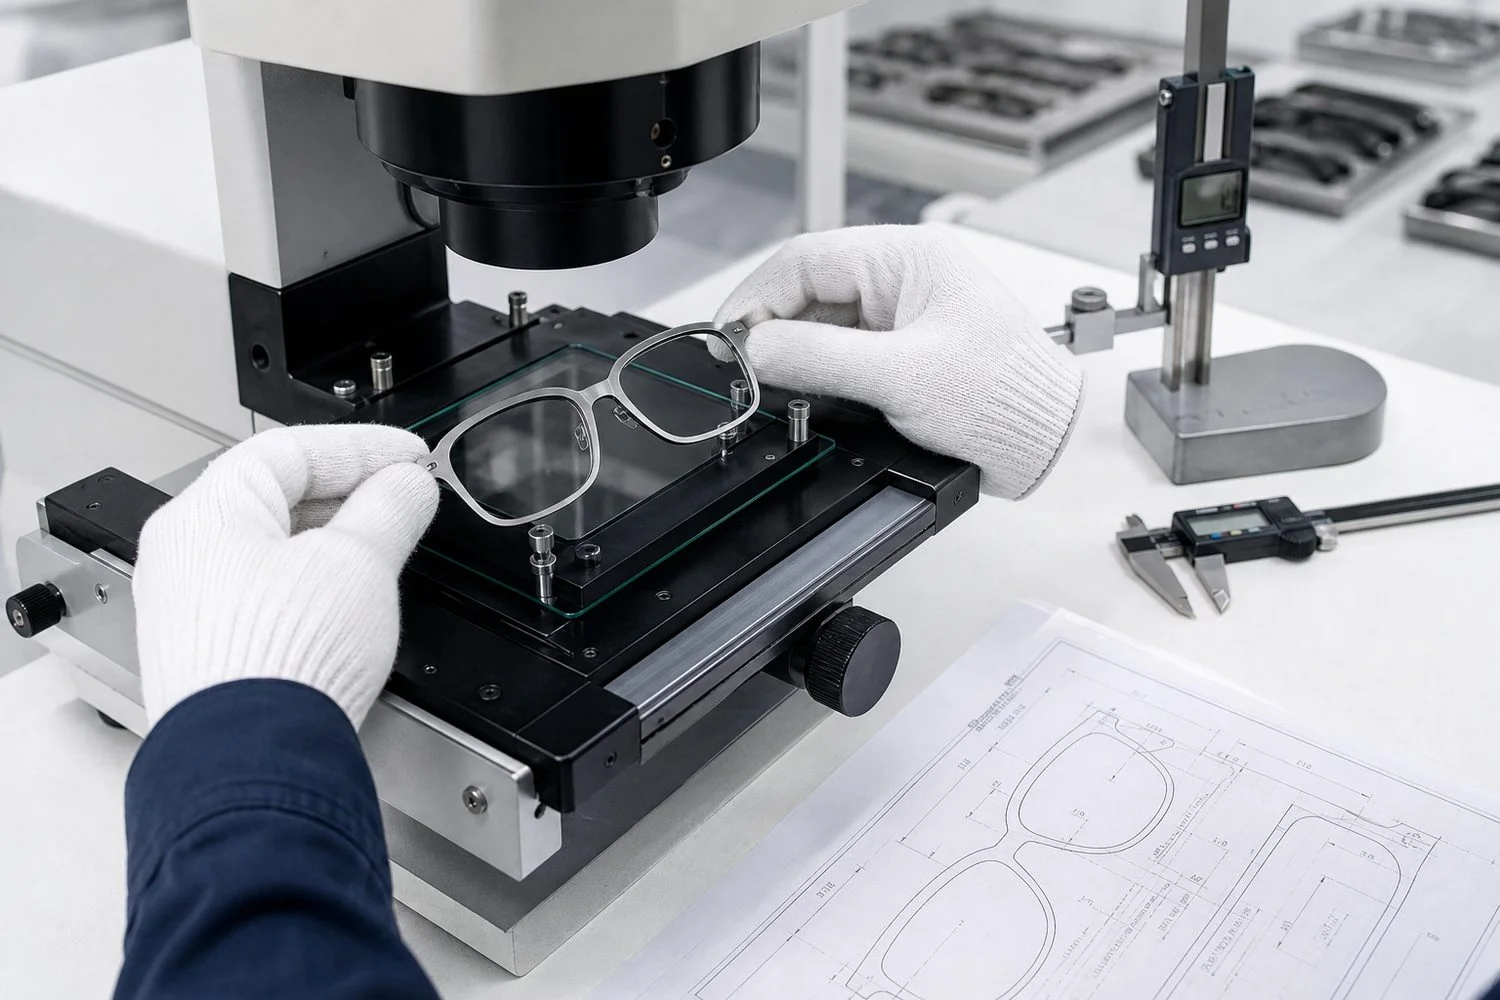
The first article checks whether the approved material, program, tools, fixture, and inspection method produce the intended part. It should report actual measured values for critical characteristics, not just a row of check marks.
Production inspection then monitors drift. Useful methods can include calibrated calipers and micrometers, pin gauges, thread gauges, optical measurement, vision systems, and coordinate measuring machines. The right method depends on feature size, geometry, tolerance, and access.
Finished frames also need product-level tests. ISO 12870:2024 specifies fundamental requirements and test methods for unglazed spectacle frames intended for prescription lenses. A precise machined component can still fail as an assembled frame if its joint, finish, adjustment, or lens retention is poor.
Why is titanium difficult to machine?
Titanium is not simply “hard.” Several material behaviors make the cutting process demanding.
Heat stays near the cutting edge
Titanium alloys conduct heat poorly compared with many common engineering metals. More cutting heat remains concentrated near the tool-chip interface. NIST researchers link the machining challenge in Ti-6Al-4V to high tool temperatures caused by low thermal conductivity and heat generated during cutting. Their infrared tool-chip study measured the interface directly.
Without controlled cutting conditions, that heat can shorten tool life and affect the surface. Check coolant delivery, tool engagement, and tool-change practices rather than relying on equipment claims alone.
Titanium can react with the cutting tool
At elevated cutting temperatures, titanium has strong chemical affinity with tool materials. Adhesion and diffusion-related wear can damage the cutting edge. A worn edge creates more heat and force, so the problem can accelerate.
The practical response is a validated combination of tool material, edge geometry, coating where suitable, cutting parameters, and coolant. There is no universal recipe for every titanium grade and frame geometry.
Thin parts can flex and vibrate
Titanium has a lower elastic modulus than steel. Thin eyewear features can spring away from the cutter or vibrate when support is poor. The result may include chatter marks, tapered walls, inconsistent thickness, or dimensional error after the part is released from the fixture.
Stable workholding, balanced stock removal, shorter tool overhang, and suitable finishing passes help. Measuring the part while it is distorted in a fixture can hide the error, so the inspection plan should define its free-state condition.
Rubbing and dwell are costly
Excess rubbing creates heat and accelerates tool wear. Interrupted cuts, small features, and poorly chosen feeds can leave the tool rubbing instead of forming a controlled chip.
A supplier should validate cutting parameters for each feature and monitor tool condition. Running the machine slowly is not, by itself, a complete titanium machining strategy.
Chips and fine dust need fire controls
A solid titanium frame is not a casual fire hazard. Fine chips and dust created during machining, grinding, or deburring are a different matter. They can be combustible and require suitable collection, housekeeping, storage, and emergency procedures.
OSHA’s combustible dust guidance identifies titanium dust incidents, and an OSHA consultation case describes wet collection designed for aluminum, titanium, and other combustible metal dusts. Buyers conducting a factory audit should include chip and dust controls, not just cosmetic housekeeping.
What are the benefits of CNC machining titanium frames?
Complex geometry without a production die
CNC milling can produce pockets, tapers, integrated details, and variable cross-sections from digital geometry. This helps with sculpted fronts and temples that would need several forming or joining operations by another route.
Fast design revision
An engineer can revise CAD and CAM data without rebuilding a full stamping die. Fixtures or programs may still need changes, so revision is not free. It is usually more direct during prototype and low-volume development.
Repeatability after the process is validated
A controlled program, fixture, tool-life plan, and measurement system can repeat features across a batch. Repeatability means the process produces similar results. Accuracy means those results match the specified target. Buyers need both.
Fewer joints for selected designs
Machining a front or temple as one piece can remove some welds or brazed joints. Fewer joints may simplify alignment and finishing. It can also increase stock consumption and cycle time, so it is a design choice rather than a universal upgrade.
Useful economics at low and medium volume
CNC can avoid a large dedicated production die for some designs. That can suit prototypes, small runs, and product families that share fixtures or stock sizes. At higher stable volumes, forming or stamping may produce a lower unit cost.
CNC machining compared with other frame processes
| Process | Best suited to | Main strength | Main limitation |
|---|---|---|---|
| CNC milling | Sculpted parts, integrated features, prototypes, low or medium volume | Digital flexibility and controlled geometry | High cycle time, stock waste, tool and fixture cost |
| Laser cutting | Flat profiles and thin sheet components | Fast profile cutting with limited mechanical force | Limited three-dimensional shaping and heat-affected edges to manage |
| Stamping and forming | Stable designs at larger volume | Short cycle time after tooling is proven | Tooling cost and slower design changes |
| Tube or wire forming | Temples, rims, bridges, and fine sections | Efficient use of slender stock | Geometry depends on forming limits and springback control |
| Additive manufacturing | Highly complex or consolidated geometry | Shape freedom and no cutting tool access limit | Surface finish, qualification, speed, and cost vary by process |
The best route may combine several processes. Ask the manufacturer to explain how each component and feature will be made. Advanced equipment cannot make up for an incomplete specification.
What drives the cost of a CNC titanium frame?
No reliable unit price can be inferred from the phrase “CNC titanium.” Cost depends on the complete production route.
Material and stock utilization
A front cut from solid plate may leave much of the purchased material as chips. This ratio of starting stock to finished part is sometimes called the buy-to-fly ratio. Better nesting, near-net preforms, and reusable standard stock can reduce waste, but they may add their own operations.
Titanium chips can have recycling value when they stay clean and separated by alloy. Recycling revenue rarely cancels the original material, machining, handling, and quality costs.
Machine and cycle time
Deep pockets, small cutters, fine finishing passes, many tool changes, and several setups add time. Five-axis equipment can reduce handling or reach complex surfaces, but its hourly cost and programming requirements may be higher.
Fixtures and setup
Custom jaws, nests, probes, and gauges create initial cost. Short runs spread that cost across fewer frames. Frequent changes in size or geometry can require new fixtures or setup validation.
Tool wear and process monitoring
Titanium machining consumes cutting tools. A supplier should plan tool changes before wear affects the finished surface. Inspection time and scrap risk also belong in the quote.
Tolerances and surface finish
Tight limits on every dimension increase machining and inspection cost even when those dimensions do not affect fit or function. Apply tight tolerances to critical features and sensible limits elsewhere.
A polished cosmetic surface may need extra stock, fine machining, manual work, and careful protection. The required finish should be shown on the drawing or an approved sample.
Lot size and revision frequency
Larger lots distribute programming, setup, and first-article work across more parts. Small color batches can still be efficient if the machined geometry stays identical. Design revisions after approval can trigger new CAM work, fixtures, samples, and inspection reports.
For the wider project view, see our guide to OEM eyewear manufacturing costs and timelines.
Buyer checklist for a CNC machining supplier
Use drawings and records to define and verify any claim of “high precision.”
Before quotation
- Identify the titanium grade, condition, and stock form by component.
- Mark functional datums and critical dimensions on a controlled drawing.
- Define cosmetic surfaces, edge breaks, burr limits, and polishing allowances.
- State order quantity, sizes, and expected revision stages.
- Ask which parts are CNC machined and which use other processes.
During process approval
- Review the proposed setup sequence and fixture concept.
- Confirm how thin rims, bridges, and temples are supported.
- Request a first-article report with actual values.
- Define the tool-change or tool-condition control for critical finishing operations.
- Confirm how parts are cleaned and protected before welding or coating.
- Review chip, dust, coolant, and fire-control practices.
Before production release
- Match the material certificate, drawing revision, program revision, and approved sample.
- Approve measurement methods for hard-to-reach or free-form features.
- Confirm in-process checks for dimensions likely to drift with tool wear.
- Inspect the part after relevant polishing or finishing, not only before it.
- Require written approval for material, program, fixture, or subcontractor changes.
- Connect component inspection to the finished-frame test plan and quality-control process.
Frequently asked questions
Is an entire titanium eyeglass frame made by CNC?
Sometimes, but rarely by CNC alone. A one-piece front and temples may be milled, while screws are turned and nose-pad arms are formed. Welding, polishing, coating, assembly, and adjustment still follow. Ask for a component-level process map.
Is a CNC-machined titanium frame stronger?
Not automatically. Strength depends on grade, condition, section thickness, grain history, stress concentrations, joints, and finishing. CNC can create a continuous one-piece shape, but poor geometry or surface damage can cancel that advantage.
What tolerance can CNC hold on an eyeglass frame?
There is no honest universal number. Capability depends on the machine, part size, geometry, tool, fixture, temperature, setup count, measurement method, and process stability. Define critical tolerances on the drawing and ask the supplier to prove them with first-article and production data.
Are visible tool marks a defect?
That depends on the approved finish. Some designs keep controlled machining marks as a visual feature. Others require polishing or coating that hides them. Define acceptable direction, depth, consistency, and reference samples before production.
Is CNC machining suitable for prototypes and mass production?
It is often strong for prototypes and low or medium volumes because programs can change without a large production die. It can also serve higher volumes when geometry, automation, fixtures, and cycle time support the economics. Compare total process cost with forming, laser cutting, and hybrid routes.
Does CNC machining waste titanium?
Subtractive machining turns some stock into chips. Good nesting, suitable stock sizes, near-net blanks, and alloy-separated recycling can reduce the impact. Buyers should compare material yield and total process steps, not just chip volume.
Specify the result, then choose the process
CNC machining can give designers control over shape and features without a dedicated production die. The outcome still depends on material selection, datums, fixtures, toolpaths, tool life, finishing, and inspection. Ask for evidence that the finished frame meets the approved requirements, not just a “CNC” label on the quote.
Developing a machined titanium style? Review our titanium eyeglass frame capabilities or contact us with your drawings, target material, quantity, finish, and critical dimensions for a structured feasibility review.